Good Manufacturing Practices

Developing, Implementing and Monitoring Good Manufacturing Practices Concepts

Last updated: 15/Oct/2026Download this page (PDF)Share this: fXin✉
In this guide
This guide breaks the subject down across the eight Food Safety & Quality system elements below — Development, Documentation, Implementation, Monitoring, Corrective & Preventative Action, Verification, Validation and Training. Select any element to explore detailed, best-practice guidance.

Premium Resources

Download our Premium Good Manufacturing Practices Resources

LOAD ALL

Downloading a resource will add this resource to your resource subscriptions. You will be notified of future updates to this resource via email (you may unsubscribe at any time by clicking the unsubscribe link in the email notification, or to unsubscribe immediately from all update notifications, click here)

To define detail, scope and purpose.

Development

This information can be used to develop food safety and quality programs that meet the requirements of modern regulatory, customer and industry standards:

  • We explain the expectations and requirements of food safety and quality compliance as they relate to your food safety and quality programs.
  • You may choose to use our Premium Resources to build, enhance or upgrade your food safety and quality program.
  • We encourage you to share this webpage with food compliance associates and peers who may benefit from our commitment to user-friendly information and resources that support a superior Food Compliance Culture.
  • We welcome your suggestions for additions of general or specific content through the haccp.com Contact page.

Key Definitions for Good Manufacturing Practices

  • Codex Alimentarius: Latin for “food code” or “food book”, a collection of internationally recognised standards, codes of practice, guidelines and other recommendations on foods, food production and food safety.
  • Cross Contact: The unintentional transfer of an allergen from one food to another.
  • Cross Contamination: The transfer of microbiological, chemical or physical contaminants from one food, surface, utensil, person or area to another.
  • Food Contact Surface: Any surface that touches food, or from which liquid or material may drain, drip or be drawn onto food, including utensils and equipment.
  • Foreign Matter: Any physical material in a food that is not part of the intended product or its packaging.
  • Good Hygiene Practices or GHP: Practices adopted to ensure appropriate levels of personal, environmental and food hygiene are maintained.
  • Good Laboratory Practices or GLP: Practices adopted to ensure appropriate levels of control are achieved within a laboratory environment.
  • Good Manufacturing Practices or GMP: Practices adopted to ensure appropriate levels of control are achieved within a food business environment.
  • Good Transport Practices or GTP: Practices adopted to ensure appropriate levels of control are achieved within a food transport environment.
  • Good Warehousing Practices or GWP: Practices adopted to ensure appropriate levels of control are achieved within a food warehouse environment.
  • Hazard Analysis Critical Control Point or HACCP: A food safety methodology that relies on the identification of Critical Control Points in all stages of food business processes.
  • Hermetically Sealed: Sealed airtight, so that air, moisture and microorganisms cannot enter.
  • Microbiological Pathogen: Any microbiological entity, including viruses, bacteria or other microorganisms, that can cause food-borne illness in humans.
  • pH: A measure of the acidity or alkalinity of a solution on a scale from 0 to 14, where 7 is neutral, values below 7 are acidic and values above 7 are alkaline.
  • Thermophilic: Describes heat tolerant bacteria that need high temperatures for normal growth.
  • Water Activity or aw: A measure of the free or unbound water in a food that is available for microbial growth. It is the vapour pressure of the food divided by the vapour pressure of pure water at the same temperature, so pure distilled water has a water activity of exactly 1.
  • Withholding Period: The minimum time between the last application of a chemical, such as a pesticide or veterinary treatment, and harvest or slaughter, so that residues fall to acceptable levels.

Good Manufacturing Practices Development

When considering the development, documentation and implementation of Good Manufacturing Practices within food safety and quality management systems, consider the following information to support effective outcomes:

About Good Manufacturing Practices

Good Manufacturing Practices (GMP) policies set out broad and specific guidelines for a food industry operation, covering:

  • Personal appearance and hygiene (see personal hygiene standards);
  • Cleaning and sanitation;
  • Food handling and manufacturing practices;
  • Other relevant industry specified requirements.

GMP policies also introduce food handlers and other people involved in the operation to appropriate workplace practices, provide documentation on hygiene, cleaning and the control of production processes within the bounds of governing legislation, and help assure that all finished food products are safe and of suitable quality. GMP are often used as the foundation for the specific food hygiene requirements of a designated sector of food production.

Every food industry sector faces particular challenges in applying GMP. The nature of the foods produced makes the results of manufacturing processes critical to consumer welfare, and failures can seriously harm consumer health. For this reason, many jurisdictions issue formal guidelines as legislation and food codes, and many require ongoing GMP training and management of food industry employees. Well-managed GMP form the basis of the prerequisite programs that support HACCP based food safety management.

The term Good Manufacturing Practices is often used alongside Good Hygiene Practices (GHP). Related variations include Good Transport Practices, Good Warehousing Practices and Good Laboratory Practices. All are bound by the requirement to produce safe and suitable outcomes against legislative requirements, industry guidelines and recognised best practice.

Both GMP and GHP commonly address:

  • Personnel practices;
  • Facility and equipment design and maintenance;
  • Process procedures;
  • Storage design and cleanliness;
  • Housekeeping;
  • General and specific cleaning and sanitation;
  • Pest control;
  • Training.

In addressing legislation, industry codes of practice and food laws, the two primary concerns of GMP and GHP are:

  • Meeting the mandatory provisions of industry codes of practice or food laws;
  • Adhering to the advisory provisions, by following an appropriate path to meet the mandatory provisions.

The Good Manufacturing Practices Policy and the Good Hygiene Practices Policy should set out what food handlers and associated people need to follow to meet these requirements.

Production Processes

Production processes aim to produce food that is safe and suitable for human consumption by:

  • Formulating design requirements for raw materials, composition, processing, distribution and consumer use for specific food items;
  • Designing, implementing, monitoring and reviewing effective food safety and quality control systems;
  • Taking preventative measures to assure the safety and suitability of food at an appropriate stage in the operation by controlling food safety and quality hazards.

Production Process Fundamentals

Consider the following in applying process control within any food business:

  • Processes should not allow the significant survival or growth of pathogenic microorganisms;
  • Food handlers must use appropriate measures to prevent contamination during preparation, storage and handling, which may include specified clothing, hand washing practices and the exclusion of staff affected by illness or injury;
  • Packaging must be made of appropriate materials and stored in a way that reduces the possibility of contamination;
  • Finished product must be stored and handled so that pathogenic microorganisms cannot survive or grow significantly;
  • Food must not be used once it has passed its use by date;
  • Food handling staff should consistently follow food hygiene protocols;
  • Equipment and premises must be properly designed, constructed, maintained, cleaned and sanitised to minimise the risk of contamination;
  • Food materials must be transported and stored at appropriate temperatures, in a manner that does not allow contamination;
  • Food handling and processing equipment must be easy to clean and sanitise before use, and constructed from impervious and non-corrodible materials;
  • Premises and equipment design should allow effective cleaning and sanitation, and be vermin proofed.

Adequate programs must be in place to monitor and control the interactions of personnel with the production of safe and suitable food, so that safe food handling practices are followed. Staff training must be verified as relevant and accurate for specific tasks, and must make people responsible for their actions within the whole process. Ongoing training, particularly in personal hygiene, personal conduct and hygienic handling of food, reinforces positive food safety outcomes.

Personnel requirements may include records of staff training and of the training content issued, and a personnel training policy covering on the job and task specific training. Refer also to process control management and training, competency and resources requirements.

The Principles of Food Hygiene

The conditions under which food is handled from production to final consumption determine its quality and safety. The basic rules for the hygienic handling, storage, processing, distribution and final preparation of food along the food production chain are set out in the Codex Alimentarius General Principles of Food Hygiene. They include requirements for design and facilities, control of operations including temperature, raw materials, water supply, documentation and recall procedures, maintenance and sanitation, personal hygiene and training of personnel.

Hygienic practices are an integral part of all food safety management systems, including HACCP. The General Principles are recommended for adoption by governments, industry (including primary producers, manufacturers, processors, foodservice operators and retailers) and consumers. They cover all circumstances necessary to ensure food safety and suitability at every stage of handling, processing, storage and distribution.

The aims of food hygiene are to:

  • Ensure food is safe to eat at the time of consumption;
  • Prevent food contamination and associated food poisoning;
  • Support the continuing effective control of food hazards, pests and other agents likely to contaminate food.

Food hygiene is achieved through effective systems that:

  • Ensure adequate maintenance, cleaning and sanitation;
  • Control pests;
  • Manage waste;
  • Monitor the effectiveness of maintenance and sanitation procedures.

Food hygiene involves:

  • Primary production: environmental hygiene, hygienic food production sources, transport, storage and handling, associated personal hygiene, cleaning and maintenance;
  • Food premises: location, design and facilities, equipment used in processing and production, maintenance, cleaning and sanitation, programmed cleaning, pest control systems, waste management, and effectiveness monitoring of all components of the food business as part of a collective system.

Key Aspects of Food Hygiene Control Systems

The aspects of food hygiene control systems below are essential to ensuring appropriate outcomes on an ongoing basis.

Primary Production

Primary production requires special attention to the identification and control of all food safety hazards, because it is most often the first step in the food supply chain. It can define the safety of the foods involved at later steps, including supply, processing and customer availability.

The control of chemical use is paramount in primary production, because chemicals such as pesticides, insecticides, fertilisers, antibiotics and fungicides are applied directly to foods or their surroundings. Residues may still be present in or on foods when they reach consumers. These hazards are controlled by following prescribed application rates and procedures, and by observing appropriate withholding periods. Refer also to chemical control.

Primary production is also the step at which foods are readily exposed to higher than acceptable levels of pathogenic bacteria, through soil, animal faeces or other environmental factors. These hazards are generally controlled through well-structured procedures that define practices supporting the production of safe and suitable foodstuffs.

Time and Temperature Control

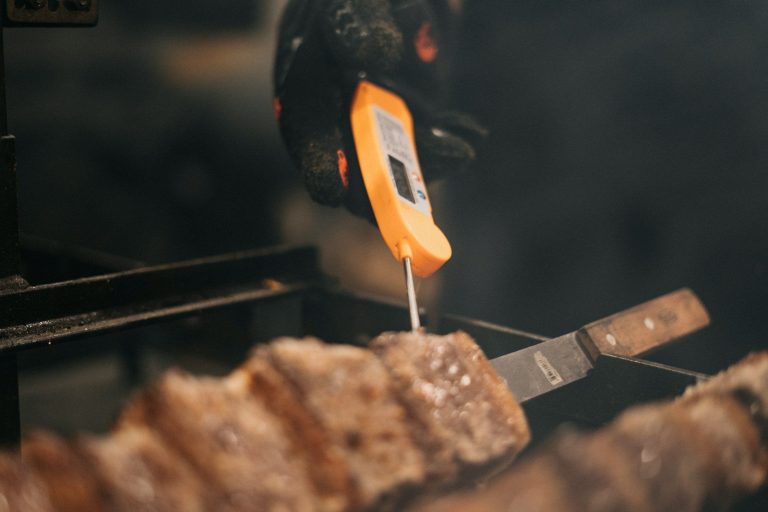
A hand holding an orange probe thermometer in cooked food to check its temperature.
Probe checks confirm that food reaches and holds safe temperatures.

Inadequate temperature control is one of the most common causes of food-borne illness and food spoilage. Controls include the time and temperature of cooking, cooling, processing and storage. Systems should ensure temperature is controlled effectively wherever it is critical to food safety and suitability.

Temperature control systems should take into account:

  • The nature of the food, for example its water activity, pH or acidity, and likely initial level and types of microorganisms;
  • The intended shelf life of the product;
  • The method of packaging and processing;
  • How the product is intended to be used, for example whether it requires further cooking or processing or is ready to eat.

Such systems should also specify tolerable limits for time and temperature variations. Temperature recording devices should be calibrated at regular intervals and tested for accuracy. Refer also to storage and handling requirements.

Specific Production Process Steps

Other steps that contribute to maintaining appropriate food hygiene outcomes may include:

  • Chilling;
  • Thermal processing;
  • Irradiation;
  • Drying;
  • Chemical preservation;
  • Modified atmosphere packaging.

As part of GMP and GHP procedures, food business management should document a policy and take all reasonable measures and precautions to address the requirements in the sections below.

Restricted Items in Specified Areas

Many materials are prohibited in food production areas because of their potential to harm consumers. The presence of the following items in production, packaging, storage and handling areas is of major concern:

  • Paper clips;
  • Rubber bands;
  • Thumbtacks;
  • Pins, nails and screws;
  • Steel wool;
  • Staples;
  • Wood: where wooden materials such as pallets must be used, keep them in a good state of repair;
  • Glass: it may be unavoidable in light fittings and instruments, but it can still be controlled through practical control measures;
  • Packaging containers: they can cause contamination during opening, either from external sources or from parts of the packaging breaking loose and contacting the food;
  • Other physical food hazards: ingredients such as dried goods can be sifted or screened before use to reduce the possibility of foreign matter moving further into the production process.

Refer also to good housekeeping practices.

Disease Control

Any person who is shown by medical examination or supervisory observation to have, or who appears to have, an illness, an open lesion (including boils, sores or infected wounds) or any other abnormal source of microbiological contamination should be excluded from any operations where there is a reasonable possibility of food, food contact surfaces or food packaging materials becoming contaminated. The exclusion should continue until the condition is corrected. Personnel should be instructed to report such health conditions to their supervisors. Refer also to personal hygiene standards.

Cleanliness

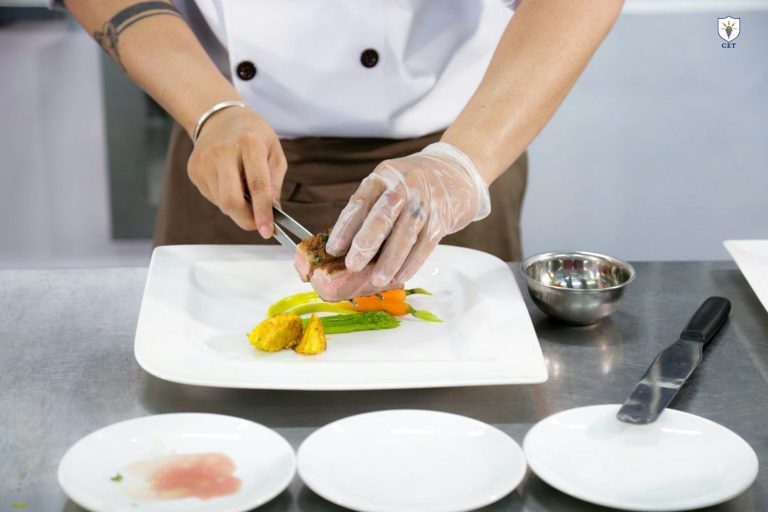
A food handler wearing disposable gloves and a white uniform prepares a dish by hand.
Clean gloves and uniforms help prevent contamination during handling.

All persons working in direct contact with food, food contact surfaces and food packaging materials should follow hygienic practices while on duty, to the extent necessary to protect against contamination of food. Methods for maintaining cleanliness include, but are not limited to:

  • Wearing outer garments suitable to the operation, in a manner that protects food, food contact surfaces and food packaging materials from contamination;
  • Maintaining adequate personal cleanliness;
  • Washing hands thoroughly, and sanitising them if necessary, in an adequate hand washing facility before starting work, after each absence from the workstation and at any other time the hands may have become soiled or contaminated;
  • Removing all unsecured jewellery and other objects that might fall into food, equipment or containers, and removing hand jewellery that cannot be adequately sanitised while food is handled by hand. If hand jewellery cannot be removed, covering it with material that can be kept intact, clean and sanitary and that effectively protects against contamination;
  • Keeping gloves, where worn, intact and clean, changing them regularly, and ensuring they are made from an impermeable food grade material;
  • Wearing hair nets, headbands, caps, beard covers or other effective hair restraints where appropriate, and storing clothing and personal belongings away from areas where food is exposed or equipment and utensils are washed;
  • Confining eating, chewing gum, drinking beverages and using tobacco to areas away from where food may be exposed or where equipment and utensils are washed;
  • Taking any other necessary precautions to protect food, food contact surfaces and food packaging materials from microorganisms and foreign substances, including perspiration, hair, cosmetics, tobacco, chemicals and medications applied to the skin.

Refer also to personal hygiene standards.

Education and Training

Personnel responsible for identifying sanitation failures or food contamination should have the education, experience or combination of both needed to produce clean and safe food. Food handlers and supervisors should receive appropriate training in food handling techniques and food protection principles, and should be informed of the dangers of poor personal hygiene and unsanitary practices.

Supervision

Responsibility for assuring compliance by all personnel with all requirements should be assigned to competent supervisory personnel.

Premises Grounds

The grounds around a food business under the control of the operator should be kept in a condition that protects against contamination of food. Methods for adequate maintenance of grounds include, but are not limited to:

  • Properly storing equipment, removing litter and waste, and cutting weeds or grass near buildings or structures that may be an attractant, breeding place or harbourage for pests;
  • Maintaining roads, yards and parking areas so they do not become a source of contamination where food is exposed;
  • Adequately draining areas that may contribute contamination to food through seepage or foot-borne filth, or that provide a breeding place for pests;
  • Operating systems for waste treatment and disposal so they do not become a source of contamination where food is exposed.

If the grounds are bordered by land that is not under the operator’s control and is not maintained in the designated manner, take care within the facility, through inspection, pest control measures or other means, to exclude pests, dirt and filth that may be a source of food contamination.

Premises Construction and Design

Buildings and structures should be suitable in size, construction and design to facilitate maintenance and sanitary operations for food manufacturing. The facility should:

  • Provide adequate ventilation or control equipment to minimise odours and vapours, including steam and noxious fumes, where they may contaminate food, and locate and operate fans and other air blowing equipment so they minimise the potential to contaminate food, packaging materials and food contact surfaces;
  • Provide, where necessary, adequate screening or other protection against pests;
  • Provide sufficient space for equipment and the storage of materials, as needed for sanitary operations and the production of safe food;
  • Permit proper precautions to reduce the potential for contamination of food, food contact surfaces or packaging materials with microorganisms, chemicals, physical contaminants or other extraneous material;
  • Be constructed so that floors, walls and ceilings can be adequately cleaned and kept clean and in good repair, drip or condensate from fixtures, ducts and pipes does not contaminate food, food contact surfaces or packaging materials, and aisles or working spaces are adequately unobstructed and wide enough for employees to perform their duties without contaminating food or food contact surfaces through clothing or personal contact;
  • Provide adequate lighting in hand washing areas, dressing and locker rooms, toilet rooms and all areas where food is examined, processed or stored and where equipment or utensils are cleaned;
  • Provide safety type light bulbs, fixtures, skylights or other glass suspended over exposed food, or otherwise protect food against contamination if glass breaks;
  • Keep food manufacturing areas and equipment used for human food separate from the manufacture of non-human animal feed or inedible products, unless there is no reasonable possibility of contaminating human food.

The potential for contamination may be reduced by adequate food safety controls and operating practices, or by effective design, including separating operations where contamination is likely to occur by one or more of the following means:

  • Location;
  • Time;
  • Partition;
  • Airflow;
  • Enclosed systems;
  • Other effective means.

Refer also to premises design and construction standards.

General Maintenance

Buildings, fixtures and other physical facilities should be kept in a sanitary condition and in sufficient repair to prevent food from becoming unsafe or unsuitable. Cleaning and sanitising of utensils and equipment should be conducted in a way that protects against contamination of food, food contact surfaces and food packaging materials.

Cleaning and sanitising chemicals and equipment should be free from undesirable microorganisms and safe and adequate for the conditions of use. Compliance may be verified by any effective means, including purchasing these substances under a supplier’s guarantee or certification and examining them for contamination.

Appropriately certified toxic materials may be used or stored in a facility where food is processed or exposed when they are:

  • Required to maintain clean and sanitary conditions;
  • Necessary for laboratory testing procedures;
  • Necessary for facility and equipment maintenance and operation;
  • Necessary for use in the facility’s operations.

Toxic cleaning compounds, sanitising agents and pesticide chemicals should be identified, held and stored in a way that protects food, food contact surfaces and food packaging materials from contamination. Follow all applicable regulations for the application, use and holding of these products. Refer also to preventative maintenance and reactive maintenance standards, cleaning and sanitation and chemical control.

Pest Control

Animals should not be allowed in any area of a food business, except assistance animals. Guard or assistance dogs may be permitted in some areas if their presence is unlikely to result in contamination of food, food contact surfaces or food packaging materials.

Take effective measures to exclude pests from processing areas and to protect food on the premises from contamination by pests. Use insecticides and rodenticides only under precautions and restrictions that protect food, food contact surfaces and food packaging materials from contamination. In general, toxic baits are laid externally, and non-toxic baits for monitoring purposes are laid in food processing and storage areas. Refer also to pest and vermin control.

Food Contact Surfaces

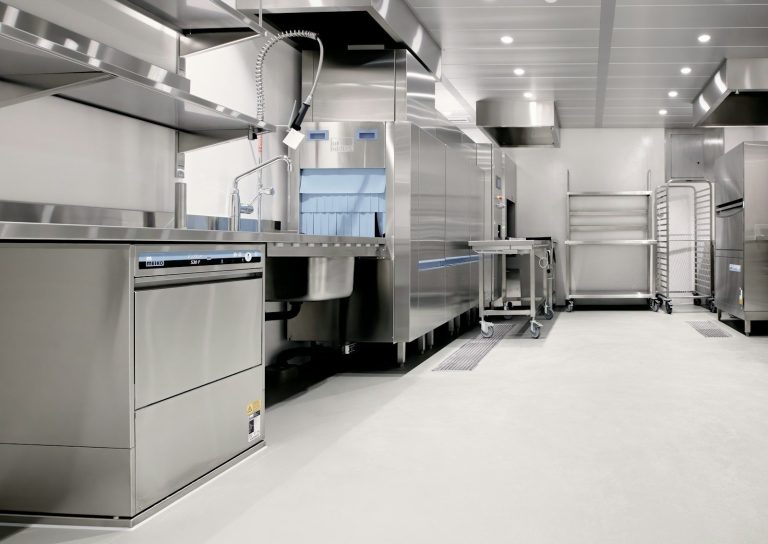
A clean commercial kitchen with stainless steel benches, shelving and a dish washing machine.
Stainless steel equipment is durable and easy to clean and sanitise.

All food contact surfaces, including utensils and the food contact surfaces of equipment, should be cleaned as frequently as necessary to protect against contamination of food.

Surfaces and materials, particularly those in contact with food, should be non-toxic, suitably durable, and easy to maintain and clean. When selecting equipment and utensils for a commercial food manufacturing facility, stainless steel is the most favoured material because it is durable and easy to clean. Wood is avoided where possible because it can harbour bacteria and tends to chip and splinter, creating a risk of physical contamination. Seams on food contact surfaces should be smoothly bonded or maintained to minimise the accumulation of food particles, dirt and organic matter, and so minimise the opportunity for microorganisms to grow.

Food contact surfaces used for manufacturing or holding low moisture food should be dry and sanitary at the time of use. When these surfaces are wet cleaned, they should, when necessary, be sanitised and thoroughly dried before subsequent use. Non food contact surfaces of equipment should be cleaned as frequently as necessary to protect against contamination of food.

In wet processing areas, when cleaning is necessary to protect against the introduction of microorganisms into food, all food contact surfaces should be cleaned and sanitised before use and after any situation in which they may have become contaminated. Where equipment and utensils are used in a continuous production operation, clean and sanitise the utensils and food contact surfaces of the equipment as necessary.

Single service articles, such as utensils intended for one time use, paper cups and paper towels, should be stored in appropriate containers and handled, dispensed, used and disposed of in a way that protects against contamination of food or food contact surfaces.

Sanitising agents should be adequate and safe under the conditions of use. Any facility, procedure or machine is acceptable for cleaning and sanitising equipment and utensils if it is established that it will routinely render them clean and provide adequate treatment.

Equipment and fittings in the manufacturing or food handling area that do not contact food should be constructed so they can be kept clean. Holding, conveying and manufacturing systems, including gravimetric, pneumatic, closed and automated systems, should be designed and constructed so they can be maintained in a sanitary condition. Refer also to equipment design and construction standards.

Storage and Handling of Equipment and Utensils

Store cleaned and sanitised equipment and utensils in a location and manner that protects food contact surfaces from contamination, for example hung, shelved with the food contact side down, wrapped or covered.

Fit each freezer and cold storage compartment used to store food capable of supporting the growth of microorganisms with an indicating thermometer, temperature measuring device or temperature recording device for monitoring purposes.

Instruments and controls used to measure, regulate or record temperatures, pH, acidity, water activity or other conditions that control or prevent the growth of undesirable microorganisms in food should be accurate and adequate in number for their designated uses. Refer also to calibration of measuring and testing equipment.

Treat compressed air or other gases mechanically introduced into food, or used to clean food contact surfaces or equipment, so that food is not contaminated with unintended contaminants.

Dropped Product

Define the requirements for any instance in which product is dropped and contacts a non-food contact surface. A dropped product policy may include corrective actions for:

  • Dropped raw materials and packaging;
  • Dropped processed product;
  • Dropped packaged product.

Consider not only the potential for physical, biological and chemical contamination of dropped product, but also damage that affects the quality of the product made available to consumers.

Raw Materials and Ingredients

Inspect and segregate, or otherwise handle, raw materials and ingredients as necessary to confirm they are clean and suitable for processing into food, and store them under conditions that protect against contamination and minimise deterioration. Wash or clean raw materials as necessary to remove soil or other contamination. Water used for washing, rinsing or conveying food should be safe and of adequate sanitary quality, and may be reused if it does not increase the level of contamination of the food. Inspect containers and carriers of raw materials on receipt to ensure their condition has not contributed to contamination or deterioration of the food.

Raw materials and other ingredients should either not contain levels of microorganisms that may cause food poisoning or other disease in humans, or should be pasteurised or otherwise treated during manufacture so that they no longer contain levels that would make the product unsafe. Compliance may be verified by any effective means, including purchasing raw materials and other ingredients under a supplier’s guarantee or certification. Refer also to approved supplier management.

Raw materials and other ingredients susceptible to contamination with aflatoxin or other natural toxins should comply with applicable food regulations and action levels for poisonous or deleterious substances before they are incorporated into finished food. Compliance may be achieved by purchasing under a supplier’s guarantee or certification, or verified by analysing these materials for aflatoxin and other natural toxins.

Thaw frozen raw materials that require thawing before use in a way that prevents other ingredients from being contaminated.

Hold liquid or dry raw materials and other ingredients received and stored in bulk in a way that protects against contamination. Items such as bulk grain, flour and oils are often kept in silos outside the facility, so product security should also be considered.

When ice is used in contact with food or as an ingredient, it should be made from safe water of adequate sanitary quality. Refer also to water and ice quality standards.

Food Packaging and Storage

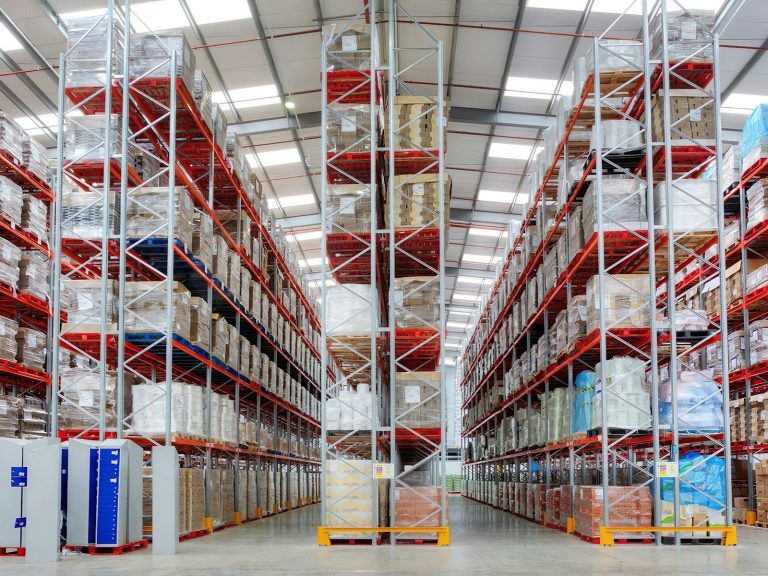
A tidy warehouse aisle with pallet racking and stored goods raised off the floor.
Orderly racked storage protects stock and supports cleaning.

Conduct packaging and storage of food under conditions and controls that minimise the potential for microbial growth and contamination. One way to comply is careful monitoring of physical factors such as time, temperature, humidity, water activity, pH, pressure and flow rate, and of manufacturing operations such as freezing, dehydration, heat processing, acidification and refrigeration, to ensure mechanical breakdowns, time delays, temperature fluctuations and other factors do not contribute to decomposition or contamination of food.

Compliance may be achieved by any effective means, including:

  • Maintaining refrigerated foods at 5°C (41°F) or below, frozen foods in a frozen state at -18°C (0°F) or below, and hot foods at 60°C (140°F) or above, as appropriate for the particular food. Required limits vary between jurisdictions and products, so confirm the limits that apply to your operation. Handle work in progress in a way that protects against contamination;
  • Heat treating or acidifying foods to destroy microorganisms when the foods are to be held in hermetically sealed containers at ambient temperatures;
  • Sterilising, irradiating, pasteurising, or controlling pH or water activity to destroy or prevent the growth of undesirable microorganisms, using measures that are adequate under the conditions of manufacture, handling and distribution to keep food safe and suitable;
  • Using sieves, traps, magnets, electronic metal detectors or X-ray machines;
  • Disposing of unsafe or unsuitable food, raw materials and ingredients in a way that protects other food from contamination. If such food can be reconditioned, use a method proven to be effective, or re-examine it and confirm it is safe and suitable before incorporating it into other food;
  • Heat blanching by heating the food to the required temperature, holding it for the required time, and then either cooling it rapidly or passing it to subsequent manufacturing without delay. Minimise thermophilic growth and contamination in blanchers through adequate operating temperatures and periodic cleaning, and use adequate time and temperature control when cooling;
  • Providing adequate physical protection of components from contaminants that may drip, drain or be drawn into them.

Perform filling, assembling, packaging and other operations in a way that protects food against contamination. Compliance may be achieved by any effective means, including:

  • Using a quality control operation in which critical control points are identified and controlled during manufacturing;
  • Adequately cleaning and sanitising all food contact surfaces and food containers;
  • Using materials for food containers and packaging that are safe and suitable under applicable packaging legislation;
  • Providing physical protection from contamination, particularly airborne contamination, and using sanitary handling procedures.

Food that relies on water activity control to prevent the growth of undesirable microorganisms, such as dry mixes, nuts, intermediate moisture food and dehydrated food, should be processed to and maintained at a safe moisture level. Compliance may be achieved by monitoring water activity and protecting finished food from moisture pickup, using a moisture barrier or other means, so water activity does not rise to an unsafe level.

Acidified food that relies principally on pH control to prevent the growth of undesirable microorganisms should be monitored and maintained at a pH of 4.6 or below. Compliance may be achieved by monitoring the pH of raw materials, food in process and finished food, and controlling the amount of acid added. Refer also to packaging standards, storage and handling requirements and validation activities.

Cross Contamination

Cross contamination can occur when pathogenic microorganisms are transferred from one food or food contact surface to another, carried by utensils, hands or other foods. Another form involves allergens, usually from improper cleaning between production runs, and is known as cross contact. Cross contamination can be controlled in the food processing environment through effective cleaning and sanitising procedures and staff participation in procedures that reduce its occurrence. Controlling cross contamination is critical where raw and ready to eat products are prepared. Refer also to allergen management.

Signage

Signage is commonly used across food industry sectors to promote food safety and quality, as well as occupational health and safety. Signage must be appropriately constructed and fitted so it does not become a food hazard. It is generally accepted that signage should be made of flexible, waterproof and cleaning chemical resistant materials. This excludes hard or brittle substances such as rigid plastic or acrylic, which could enter foods as physical hazards.

When signage refers to procedures, policies or other components of the documented food safety and quality system, it should reference their content. Include the signage in a register, for example the document register, so it is amended whenever the associated policies or procedures are amended. Refer also to document and data control.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Development requirements in relation to their items.

References

The following references provide further guidance on food hygiene and prerequisite programs. Refer to the current edition of each.

Good Manufacturing Practices Development Key Points

  • Good Manufacturing Practices programs must be developed to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • Senior Management of your business facilitates a commitment to providing adequate resources for the development of your Good Manufacturing Practices program;
  • If you require additional resources for the development of Good Manufacturing Practices program elements, discuss this with the relevant Senior Management representative;
  • A properly developed Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly developed Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To establish the developed detail in a viewable format to facilitate information.

Documentation

Document: A document provides guidance and/or direction for performing work, making decisions, or rendering judgments that affect the safety or quality of the products or services that customers receive.

Documented policies, procedures, work instructions, and schedules form the basis of any food safety and quality management system. The following documentation formats may be considered to ensure ongoing compliance with specified requirements for Good Manufacturing Practices:

  • Good Manufacturing Practices policy;
  • Good Manufacturing Practices development procedures;
  • Good Manufacturing Practices implementation procedures and work instructions;
  • Good Manufacturing Practices monitoring procedures;
  • Good Manufacturing Practices corrective and preventative action procedures;
  • Good Manufacturing Practices verification schedule;
  • Good Manufacturing Practices verification procedures;
  • Good Manufacturing Practices validation schedule;
  • Good Manufacturing Practices validation procedures;
  • Good Manufacturing Practices training procedures.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Documentation requirements in relation to their items.

You may wish to visit the Good Manufacturing Practices Templates section of haccp.com for examples of Good Manufacturing Practices documentation, record, and resource formats commonly applied within food safety and quality systems.

Good Manufacturing Practices Documentation Key Points

  • Good Manufacturing Practices programs must be documented to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • All documented Good Manufacturing Practices program elements must be controlled to ensure compliance;
  • Key documented Good Manufacturing Practices program elements should be available to your business team at all times to ensure they can facilitate required tasks;
  • A properly documented Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly documented Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To facilitate the application of the documentation.
Implementation

Implementation: Implementation is the application of documented food safety and quality system elements into the actual business operation. The implementation of Good Manufacturing Practices within any food business requires genuine commitment from senior management, staff and visitors to ensure the nominated goals of implementation are achievable on an ongoing basis. It is a step that requires significant planning and consideration of general and specific food business circumstances to ensure the outcomes of Good Manufacturing Practices do not negatively impact the safety and quality of the food items dispatched from the business.

Implementation of Good Manufacturing Practices must include a clear definition of responsibilities and authorities for all levels of participation by senior management, staff and visitors to the site.

When implementing Good Manufacturing Practices within a food safety and quality system, you may wish to consider the following requirements before completion:

  • Communication and display of the Good Manufacturing Practices policy;
  • Completion of Verification and Validation of Good Manufacturing Practices development procedures;
  • Availability of Good Manufacturing Practices implementation procedures and work instructions;
  • Availability of Good Manufacturing Practices monitoring procedures and record templates where applicable;
  • Availability of Good Manufacturing Practices corrective and preventative action procedures and record templates where applicable;
  • Availability of the Good Manufacturing Practices verification schedule;
  • Availability of Good Manufacturing Practices verification procedures;
  • Availability of the Good Manufacturing Practices validation schedule;
  • Availability of Good Manufacturing Practices validation procedures;
  • Completion of Good Manufacturing Practices training procedures;
  • Completion of product design and development requirements related to Good Manufacturing Practices;
  • Completion of process design and development requirements related to Good Manufacturing Practices;
  • Completion of training for team members who have responsibilities and involvement within Good Manufacturing Practices;
  • Completion of competency approval for team members who have responsibilities and involvement within Good Manufacturing Practices.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Implementation requirements in relation to their items.

Good Manufacturing Practices Implementation Key Points

  • Good Manufacturing Practices programs must be implemented to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • Your Good Manufacturing Practices program must be fully implemented as per relevant documented Policies, Procedures, and Work Instructions;
  • The implementation of Good Manufacturing Practices requires a commitment to the provision of resources by the Senior Management of your business;
  • A properly implemented Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly implemented Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To review, confirm and document evidence of the implementation against documented limits.

Monitoring

Monitoring: Monitoring is the act of reviewing and confirming measurable parameters of a defined process or product status.

Monitoring requirements within food industry sectors are generally identified against limits of acceptability defined within HACCP plans, implementation procedures, and work instructions. Monitoring usually includes some element of record-keeping, which may be maintained manually or through digital systems. It is important to consider that advancements in technology have spawned many systems and processes which are self-monitored or self-adjusting when variances are identified. Regardless of the system used, the goal of any monitoring activity is to provide sufficient evidence that any limit of acceptability has been met.

Traditional Good Manufacturing Practices monitoring requirements include manual recording and the application of corrective actions when the results of monitoring are found to be outside acceptable limits. Corrective Actions should also generally be strongly linked to the monitoring process where applied to ensure full traceability of the applied actions.

Common Good Manufacturing Practices monitoring activities and records include:

  • Pre-operational inspection records, which are scheduled, conducted and recorded to confirm that cleaning and sanitation, premises and equipment, and allergen management controls have been completed as specified. Allergen swabs, or methods such as ATP bioluminescence swabbing, are often used as real time verification within pre-operational inspections;
  • Daily pre-operational checks, which allow management and staff to confirm that all items are clean, sanitised and suitably stored before production starts;
  • Personal hygiene and hand washing checks;
  • Temperature checks of storage, processing and cooling;
  • Pest activity inspections;
  • Foreign matter checks and dropped product records;
  • Routine monitoring of GMP prerequisite programs across the premises.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Monitoring requirements in relation to their items.

You may wish to visit the Good Manufacturing Practices Templates section of haccp.com for examples of Good Manufacturing Practices documentation, record, and resource formats commonly applied within food safety and quality systems.

Good Manufacturing Practices Monitoring Key Points

  • Monitoring provides real-time confirmation and evidence that your risk-based FS&Q Controls are effectively implemented;
  • Good Manufacturing Practices programs must be monitored to meet relevant Regulatory, Industry, and Customer standards and requirements;
  •  Monitoring of Good Manufacturing Practices must be facilitated as per relevant documented Policies, Procedures, and Work Instructions;
  • Nominated monitoring records for Good Manufacturing Practices must be maintained as per relevant documented Policies, Procedures, and Work Instructions;
  • A properly monitored Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly monitored Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To apply “real time” interventions to documented monitoring limits.

Corrective Action and Preventative Action

Corrective Action: Corrective action is mandatory action to be taken when a deviation to the Quality System occurs, particularly with a Critical Control Point.

Preventative Action: At any step in the process where a hazard has been identified, preventative action must be put into place to prevent re-occurrence.

Corrective Action and Preventative Action are implemented to ensure that any identified non-conformance issues are documented, investigated, and rectified within appropriate time frames. Corrective action is any action applied to regain control over a product, process, policy, or procedure that has been identified as being non-conforming or outside nominated limits of acceptability. Preventative action is any action applied to prevent any identified non-conformance from reoccurring.

The outcomes of corrective and preventative actions should result in regained process control after effective application. Specified corrective actions are commonly linked to the HACCP Plans and the food business certification process.

Below are Corrective Action and Preventative Action examples which may be associated with Good Manufacturing Practices related non-conformance:

  • Review of the Good Manufacturing Practices policy;
  • Review of Good Manufacturing Practices development procedures;
  • Review of Good Manufacturing Practices implementation procedures and work instructions;
  • Review of Good Manufacturing Practices monitoring procedures;
  • Review of Good Manufacturing Practices corrective and preventative action procedures;
  • Review of the Good Manufacturing Practices verification schedule;
  • Review of Good Manufacturing Practices verification procedures;
  • Review of the Good Manufacturing Practices validation schedule;
  • Review of Good Manufacturing Practices validation procedures;
  • Review of Good Manufacturing Practices training procedures;
  • Re-training in Good Manufacturing Practices;
  • Review of management review activities to include Good Manufacturing Practices as an agenda item;
  • Initiation of ‘product hold’ procedures where safety or quality may be compromised;
  • Initiation of a product recall or product recall procedures where investigations show that there is a substantial safety or quality risk to the released product;
  • Contacting stakeholders including customers regarding any confirmed or potential Good Manufacturing Practices concerns involving their product.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Corrective Action requirements in relation to their items.

You may wish to visit the Corrective Action and Preventative Action section of haccp.com for examples of best practice applications for this food safety and quality system element.

Good Manufacturing Practices Corrective Action and Preventative Action Key Points

  • The implementation of Corrective Action and Preventative Action provides confidence that your FS&Q Program is effectively implemented and that FS&Q criteria are being met;
  • Where deviations or variations are observed, Corrective Actions and Preventative Actions must be facilitated to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • Corrective Action and Preventative Action of Good Manufacturing Practices must be facilitated as per relevant documented Policies, Procedures, and Work Instructions;
  • Records of Corrective Action and Preventative Action for Good Manufacturing Practices must be maintained per relevant documented Policies, Procedures and Work Instructions;
  • Proper application of Corrective Action and Preventative Action for your Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • Poor application of Corrective Action and Preventative Action for your Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To review and confirm documented monitoring and corrective actions against documented parameters.

Verification

Verification: The act of reviewing, inspecting, testing, checking, auditing, or otherwise establishing and documenting whether items, processes, services, or documents conform to specified requirements.

Verification is the detailed review of all food safety and quality system elements to confirm that they are effectively developed, documented, implemented, monitored, and reviewed. All food safety and quality system elements, including documented policies, procedures, training, HACCP plans, and their operational applications must be verified on an ongoing scheduled basis. The verification process commonly includes a defined schedule for which verification activities are required, how often they are conducted, who is responsible, and detailed documented procedures for each nominated verification activity.

The general goal of an established verification process is to ensure any systemic non-conformance issues are identified and rectified within an appropriate time frame. When non-conformance issues are identified through the verification process, Corrective Actions and Preventative Actions should be implemented to ensure they do not impact the effectiveness of the food safety and quality system.

The following examples of verification activities may apply to Good Manufacturing Practices:

  • Review of the Good Manufacturing Practices policy;
  • Review of Good Manufacturing Practices development procedures;
  • Review of Good Manufacturing Practices implementation procedures and work instructions;
  • Review of Good Manufacturing Practices monitoring procedures;
  • Review of Good Manufacturing Practices monitoring records;
  • Review of Good Manufacturing Practices corrective and preventative action procedures;
  • Review of the Good Manufacturing Practices verification schedule;
  • Review of Good Manufacturing Practices verification procedures;
  • Review of the Good Manufacturing Practices validation schedule;
  • Review of Good Manufacturing Practices validation procedures;
  • Review of Good Manufacturing Practices training procedures;
  • Review of Good Manufacturing Practices performance since the last review and historically;
  • Analytical testing of product or process to ensure the effectiveness of Good Manufacturing Practices;
  • Inclusion of Good Manufacturing Practices as an agenda item within the Management Review Process.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Verification requirements in relation to their items.

You may wish to visit the Verification Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.

Good Manufacturing Practices Verification Key Points

  • Your verification program provides evidence that your FS&Q Controls have worked;
  • Good Manufacturing Practices programs must be verified to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • The verification of Good Manufacturing Practices must be facilitated as per relevant documented Policies, Procedures and Work Instructions;
  • Nominated verification records for Good Manufacturing Practices must be maintained as per relevant documented Policies, Procedures, and Work Instructions;
  • A properly verified Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly verified Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

To confirm the documented monitoring or procedural limits.

Validation

Validation: The process of gathering evidence to provide a scientific basis for the documented act of demonstrating that a procedure, process, and activity will consistently lead to the expected results. It often includes the qualification of systems and equipment.

Validation is the provision of evidence to support the limits of control or acceptability for food safety or quality parameters nominated within systemic elements. Limits of control or acceptability are commonly included within documented food safety and quality systems elements such as procedures, HACCP plans, and specifications.

Common sources of validation include regulatory and legislative standards, finished product specifications and customer requirements, industry codes of practice and guidelines, verified and validated research, historical product, and process control outcomes, and analytical testing.

The general goal of an established validation process is to ensure any systemic non-conformance issues are identified and rectified within an appropriate time frame. When non-conformance issues are identified through the validation process, Corrective Actions and Preventative Actions should be implemented to ensure they do not impact the effectiveness of the food safety and quality system.

Validation activities are commonly defined within the verification schedules and procedures of established food safety and quality management systems.

The following examples may apply to validation of the limits of control or acceptability for Good Manufacturing Practices:

  • Confirmation of nominated food safety and food quality control limits for Good Manufacturing Practices. These limits may apply to regulatory, industry, customer, or finished product specifications;
  • Confirmation of analytical testing methods being used to confirm the effectiveness of Good Manufacturing Practices and ensure the accuracy of outcomes.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Validation requirements in relation to their items.

You may wish to visit the Validation Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.

Good Manufacturing Practices Validation Key Points

  • Your validation program provides evidence that your FS&Q Controls will work;
  • Good Manufacturing Practices programs must be validated to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • The validation of Good Manufacturing Practices must be facilitated as per relevant documented Policies, Procedures, and Work Instructions;
  • Nominated validation records and supporting documentation for Good Manufacturing Practices must be maintained as per relevant documented Policies, Procedures, and Work Instructions;
  • A properly validated Good Manufacturing Practices program will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • A poorly validated Good Manufacturing Practices program will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

Skills, knowledge and competency requirements to facilitate development, documentation, implementation, monitoring, corrective action, verification and validation of every Food Safety and Quality System Element.

Skills and Knowledge

Skills and Knowledge: Skills and knowledge are attributes of human interactions commonly linked to competency within any specified job-related task.

Training and competency requirements for Good Manufacturing Practices must be ongoing, including regularly scheduled reviews to ensure the effectiveness of training and competency outcomes.

Team members who have defined responsibilities regarding Good Manufacturing Practices should have knowledge including:

  • Basic Good Manufacturing Practices requirements;
  • Positive outcomes of Good Manufacturing Practices;
  • Negative outcomes of a lack of Good Manufacturing Practices;
  • Current Good Manufacturing Practices procedures, methods, and techniques;
  • General operational, corporate, and social awareness regarding Good Manufacturing Practices;
  • Regulatory, industry, and customer requirements regarding Good Manufacturing Practices.

Team members who have defined responsibilities regarding Good Manufacturing Practices should have skills including:

  • Competency regarding basic Good Manufacturing Practices;
  • Effective application of current Good Manufacturing Practices procedures, methods, and techniques;
  • The basic development, documentation, and implementation of HACCP and Prerequisite Programs within the food industry sector.

Team members who have defined responsibilities regarding Good Manufacturing Practices should have access to resources including:

  • Good Manufacturing Practices training;
  • Good Manufacturing Practices associations and events;
  • Regulatory standards, industry and customer information and updates regarding Good Manufacturing Practices;
  • Incidents within the food industry sector regarding Good Manufacturing Practices;
  • Commitment to Good Manufacturing Practices by senior management;
  • Suitably qualified food industry professionals with verified experience in Good Manufacturing Practices;
  • Effective communication systems including email, internet, and phone through which Good Manufacturing Practices information can be sent and received within suitable timeframes.

If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Good Manufacturing Practices Training, Competency, and Resources requirements in relation to their items.

You may wish to visit the Training, Competency and Resources section of haccp.com for examples of best practice applications for this food safety and quality system element.

Good Manufacturing Practices Training, Skills and Knowledge Key Points

  • Your Training, Skills, and Knowledge program ensures all participating personnel, visitors and contractors have the required skills and knowledge to effectively facilitate the requirements of your FS&Q Program;
  • Training, Skills and Knowledge programs for Good Manufacturing Practices must be facilitated to meet relevant Regulatory, Industry, and Customer standards and requirements;
  • Training, Skills and Knowledge programs for Good Manufacturing Practices must be facilitated as per relevant documented Policies, Procedures, and Work Instructions;
  • Training, Skills, and Knowledge records for Good Manufacturing Practices must be maintained as per relevant documented Policies, Procedures and Work Instructions;
  • Properly applied Training, Skills, and Knowledge programs for Good Manufacturing Practices will provide a strong framework for your business to maintain compliance with relevant Regulatory, Industry, and Customer standards and requirements;
  • Poorly applied Training, Skills, and Knowledge programs for Good Manufacturing Practices will not fully support your business and may contribute to significant non-compliance against Regulatory, Industry, and Customer standards and requirements.

Share this:

Facebook
Twitter
X
Email