

To define detail, scope and purpose.
To establish the developed detail in a viewable format to facilitate information.
To facilitate the application of the documentation.
Downloading a resource will add this resource to your resource subscriptions. You will be notified of future updates to this resource via email (you may unsubscribe at any time by clicking the unsubscribe link in the email notification, or to unsubscribe immediately from all update notifications, click here)
Downloading a resource will add this resource to your resource subscriptions. You will be notified of future updates to this resource via email (you may unsubscribe at any time by clicking the unsubscribe link in the email notification, or to unsubscribe immediately from all update notifications, click here)
This information can be used to develop food safety and quality programs that meet the requirements of modern Regulatory, Customer and Industry Standards:
When considering the development, documentation, and implementation of Commercial Sterility Processing within food safety and quality management systems, the following information should be considered to ensure effective outcomes:
Commercial sterility techniques have been used since the early 19th century to preserve foods. Early techniques involved sealing foods into glass bottles and boiling the bottles in water for extended timeframes. By the mid-19th century, tin-coated steel containers were being used in what would become one of the most prevalent food preservation techniques used throughout the world.
Commercial sterility techniques are well suited to preserving foods as they kill and deactivate microorganisms and their spores through structured process controls involving the creation of an anaerobic environment and time and temperature treatments.
Microorganisms, many of which are harmful to humans, are also responsible for the spoilage of foods. Applying a suitable temperature to foods over a defined period denatures proteins and enzymes, which are essential components of living cells. This damage kills vegetative bacteria, which is the simpler part of the commercial sterility process. The challenge is to kill bacterial spores, which are more robust than vegetative bacteria. Bacterial spores are difficult to kill because they have thick protective walls which increase their resistance to heat, drying, freezing, chemicals, and radiation. The ‘kill step’ for bacterial spores widely defines the modern parameters for Commercial Sterility.
Modern Commercial Sterility techniques include retorting, static aseptic, and continuous flow applications:
The goal of all variants of Commercial Sterility is to produce foods that remain sterile whilst their packaging remains intact.
The pH of a food determines how much heat processing is required. Low-acid foods have a finished equilibrium pH above 4.6 and a water activity above 0.85, which allows Clostridium botulinum spores to germinate and produce toxin in the anaerobic, non-refrigerated conditions inside a sealed container. For this reason, low-acid canned foods are given a severe heat treatment, commonly expressed as an F0 value (equivalent minutes at 121.1°C (250°F)), which delivers a very high reduction in Clostridium botulinum spores.
Acidified foods are low-acid foods to which acid is added to bring the finished equilibrium pH to 4.6 or below. Acidic conditions prevent spore germination, so a milder heat treatment is typically used, and control of pH becomes a critical parameter. Naturally acidic foods, such as many fruits, are also commonly processed using a milder heat treatment.
Scheduled processes for low-acid and acidified foods should be established by a process authority and supported by heat penetration studies for each product, container size and retort type.
A D-value is the specific time required at a specific temperature to kill, for example, 90% of bacterial spores, which is the same as reducing their number by one logarithm unit. In short, the D-value is a measure of the heat resistance of a specified type of bacteria. The D-value depends on the species of bacterial spores involved.
The outcome of any heat sterilisation process depends heavily on the following factors:
Commercial Sterility Processing relies on one or more steps at which microorganisms are killed and their spores destroyed. When applying a sterilisation procedure such as heat, not all bacterial spores are killed at the same time. A certain proportion of spores is killed within any given period at a suitable temperature, but not all of them.
This is where the most important factor of Commercial Sterility Processing comes to the forefront: lethality depends on both temperature and time. At a given temperature, the time required to achieve the target reduction is what the process is designed around, and a higher temperature shortens that time.
The process through which time and temperature are used to kill bacteria is commonly known as logarithmic reduction. Because each log reduction removes a fixed proportion of the remaining spores, the count can approach zero but never reach it, so it is never possible to guarantee absolute sterility. In this context, the efficiency of sterilisation is expressed by the number of decimal reductions in the count of bacterial spores. The D-value, or Decimal Reduction Time, is commonly used to indicate the killing rate of bacterial spores.
In some applications, more than one temperature and time combination is applied to achieve the required sterilisation, increasingly to maintain product quality. In such instances, the required change in temperature is described by the Z-value, which is defined as the change in temperature required to alter the D-value by a factor of one logarithmic unit.
As absolute sterility is not achievable, sampling plans with nominated acceptable tolerances are commonly defined for displaying conformance with the method of Commercial Sterility Processing employed.
A common example of a sampling plan applied for Commercial Sterility Processing is a maximum acceptable defect rate of 1 in 10,000 samples. To determine the effectiveness of the Commercial Sterility Processing methods employed, and to ensure the number of defects does not exceed the nominated target, sampling procedures are implemented.
It is common for a defined sample percentage of finished products from each batch to undergo an ‘incubation’ process to ascertain the absence of microorganisms within finished products. This supports the effectiveness of the time and temperature controls of each processed batch of product. Incubations are commonly conducted at 37°C (99°F), a temperature favourable to the growth of any potential microorganisms contained within the processed product. Incubation temperatures and durations for mesophilic and thermophilic organisms are defined by the applicable regulation, customer requirement or process authority. Generally, if the incubated products do not show any signs of bloating or loss of vacuum, it is assumed that the Commercial Sterility process has been successful.
As the methods and techniques used for Commercial Sterility Processing are long-established, and have a strong validated and verified history of achieving their intended food safety goals under controlled conditions, products are commonly not required to be microbiologically tested on a scheduled basis. Though the Commercial Sterility process should always achieve consistent results when conducted in a controlled and verified manner, it is important to consider that analytical microbiological testing can provide substantial evidence of product conformance to Commercial Sterility standards. In this context, it is of utmost importance for the analytical microbiological testing of commercially sterile products, when conducted, to ensure that the product within its original packaging is not contaminated as an element of the sampling or testing process.
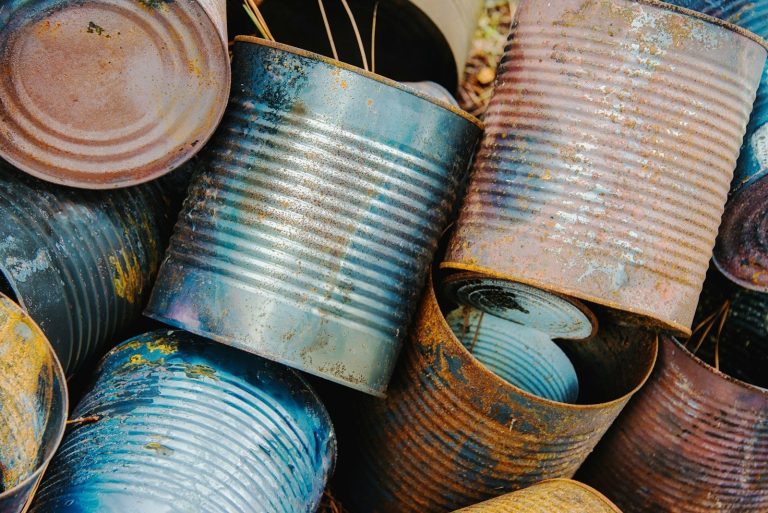
Packaging materials used in the canning process are made from a thin steel strip coated with a thin layer of tin on the internal and external surfaces. In many cases, the interior of cans is lined with an organic compound to separate the food from the tin lining and prevent any chemical reaction. A rubber-like compound helps to form a hermetic seal when the bottom and lid are seamed onto the body of the can.
Once canned food is produced, poor transportation or storage practices might cause denting or damage to the can seams. Leaks resulting from damage can allow contamination to enter the can, which may allow spoilage to occur. Poor handling and storage conditions over time may also result in rusting of the outside of the can. Rusting commonly occurs when cans are stored in high humidity conditions, and is normally just unsightly, but can cause leakage over extended periods.
Badly dented cans, particularly those with damage to the double seam, should be rejected or placed on hold, and the cause investigated. Bulging can ends may indicate microbial growth and a significant risk to consumers, so affected cans should be isolated unopened and returned to the supplier or managed as non-conforming product. Cans with stained labels may indicate poor storage practices and a possible leak, and should also be rejected if identified. Consumers who find damaged cans should return them unopened to the store of purchase.
The hermetically sealed contents of canned food are uncontaminated before opening, so great care should be taken to ensure contaminants are not introduced when the can is opened. It is considered best practice for the top of the can to be washed before opening. This will ensure that any dust or dirt on the can top will not enter the food during the opening process.
When opening canned food, a clean, sharp can opener should be used. Because the metals used in the construction of the can are relatively soft, the use of a blunt can opener can introduce small pieces of metal into the food contained within the can. Blunt can openers also leave jagged edges, which can provide health and safety risks. Can openers should ideally be washed after each use to further avoid the risk of contamination.
Once opened, canned foods should be treated as fresh foods. After opening, foods should be immediately removed from their can, placed into a non-reactive container with a tight-fitting lid, and stored within a refrigerator. Opened canned foods should be used within a suitable timeframe, as they will spoil after the hermetic seal on the can has been breached.
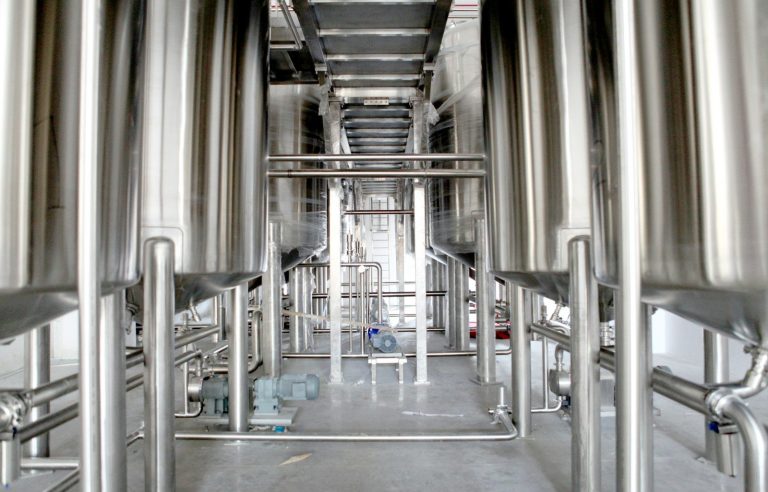
Aseptic processing and packaging is a complex technique as it relies on a minimum of three different sterilisation techniques to be effective.
As elements of aseptic processing and packaging methods, sterilisation is conducted:
Failure of any one of these three techniques may result in an unsafe end product. Sterilisation of equipment must also be supported by effective cleaning and sanitation before it begins. In this context, potential microbiological contamination points within an aseptic packaging facility must be addressed in a holistic sense.
For example, in a canning operation, if the product or package is contaminated before the retorting process, all bacteria and spores will be destroyed through the time and temperature process for the sealed can. In a similar instance within aseptic packaging, where the product or packaging was not sanitary, the result would be an unsafe product, as there are no further kill steps after the product has been packaged.
Flexible packaging for commercially sterile food products is becoming increasingly popular due to its versatility and shorter processing times, which can be reduced dramatically compared to rigid packaging such as cans. Additional advantages for manufacturers include reduced shipping costs and storage space for empty flexible packaging, such as pouches. Whilst flexible commercially sterile packaging has advantages, challenges include seal integrity and the need for more complex filling systems. Its thin profile also allows heat to penetrate faster than in cans, which shortens the heat processing time required to achieve commercial sterility.
A typical commercially sterile pouch is a heat-resistant bag made of laminated plastic films or foil, commonly consisting of an outer layer of polyester or nylon for printing, coding and protection, a middle aluminium foil layer that functions as the principal oxygen and water vapour barrier, and an inner or food contact layer of a heat sealant material such as polypropylene. Products are filled aseptically and sealed, or sealed and sterilised by pressure cooking in a retort, to produce commercially sterile finished products.
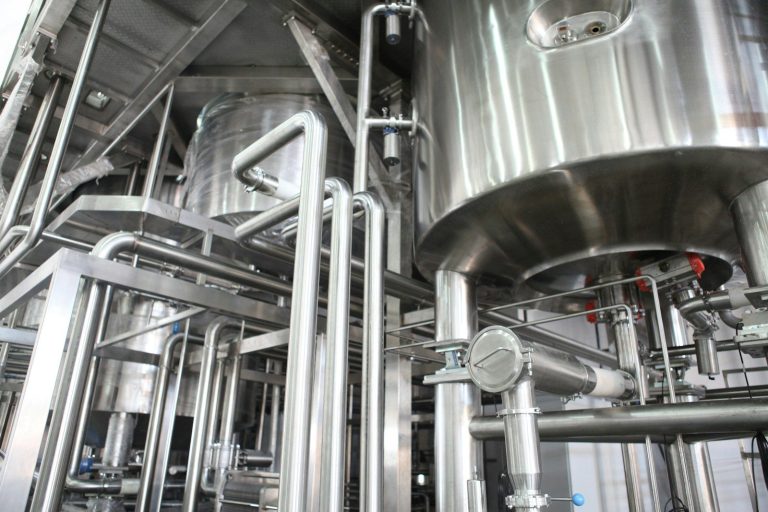
There are two main modern UHT processing methods used within food industries: direct heating and indirect heating. Both methods apply heat to the product at a high temperature for a short time. The method selected relies on the nature and volume of the product being treated.
Direct heating usually involves subjecting the product to steam under controlled conditions until a nominated temperature is achieved for a nominated timeframe, after which the product is rapidly cooled within a vacuum vessel. Rapid heating and cooling gives a minimal sustained heat load on the product, which results in a high-quality end product.
Indirect heating involves circulating the product around partitions that are themselves heated or cooled according to the relevant process. The heating or cooling medium on the non-product contact side of the partition transfers its heat or chill to the product without physically contacting it. The equipment used to heat the product within this method is commonly referred to as a heat exchanger.
Heat exchangers are commonly available in three different types:
Water is commonly used in the initial cooling of commercially sterile products. Any water used for product cooling must be chlorinated or otherwise treated so that it will not introduce microbiological pathogens into foods during the cooling process.
This is particularly important for canned products, as cans expand and contract during temperature and pressure variations, and contamination may enter at the can seams or ends. If water used to cool retorted items is adequately treated, it will not contaminate the product inside the can. The Codex Code of Hygienic Practice for Low and Acidified Low Acid Canned Foods considers a residual free chlorine content of 0.5 to 2 parts per million (ppm) to be usually adequate for cooling water.
Additional cooling is commonly facilitated after the items have been removed from the retort within a well-ventilated area. Containers remain wet and vulnerable to seam contamination until dry, so handling of wet containers should be minimised and equipment that contacts them kept clean.
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Development requirements in relation to their items.
Commercial sterility requirements vary by market, and the following references may assist in the development of your program:
Customer requirements and the advice of your process authority may also apply to your Commercial Sterility Processing program.
Document: A document provides guidance and/or direction for performing work, making decisions, or rendering judgments that affect the safety or quality of the products or services that customers receive.
Documented policies, procedures, work instructions, and schedules form the basis of any food safety and quality management system. The following documentation formats may be considered to ensure ongoing compliance with specified requirements for Commercial Sterility Processing:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Documentation requirements in relation to their items.
You may wish to visit the Commercial Sterility Processing Templates section of haccp.com for examples of Commercial Sterility Processing documentation, record, and resource formats commonly applied within food safety and quality systems.
Implementation: Implementation is the application of documented food safety and quality system elements into the actual business operation.
The implementation of Commercial Sterility Processing within any food business requires genuine commitment from senior management, staff, and visitors to ensure the nominated goals of implementation are achievable on an ongoing basis. It is a step that requires significant planning and consideration of general and specific food business circumstances to ensure the outcome of Commercial Sterility Processing does not negatively impact the safety and quality of the food items dispatched from the business.
Implementation of Commercial Sterility Processing must include a clear definition of responsibilities and authorities for all levels of participation by senior management, staff, and visitors to the site.
When implementing Commercial Sterility Processing within a food safety and quality system, you may wish to consider the following requirements before completion:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Implementation requirements in relation to their items.
Monitoring: Monitoring is the act of reviewing and confirming measurable parameters of a defined process or product status.
Monitoring requirements within food industry sectors are generally identified against limits of acceptability defined within HACCP plans, implementation procedures, and work instructions. Monitoring usually includes some element of record-keeping, which may be maintained manually or through digital systems. It is important to consider that advancements in technology have produced many systems and processes that are self-monitored or self-adjusted when variances are identified. Regardless of the system used, the goal of any monitoring activity is to provide sufficient evidence that any limit of acceptability has been met.
Traditional Commercial Sterility Processing monitoring requirements include manual recording and the application of corrective actions when the results of monitoring are found to be outside acceptable limits. Corrective Actions should also generally be strongly linked to the monitoring process where applied to ensure full traceability of the applied actions.
The following examples of monitoring activities and record formats may apply to Commercial Sterility Processing:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Monitoring requirements in relation to their items.
You may wish to visit the Commercial Sterility Processing Templates section of haccp.com for examples of Commercial Sterility Processing documentation, record, and resource formats commonly applied within food safety and quality systems.
Corrective Action: Corrective action is mandatory action to be taken when a deviation from the Quality System occurs, particularly in relation to a Critical Control Point.
Preventative Action: At any step in the process where a hazard has been identified, preventative action must be put into place to prevent re-occurrence.
Corrective Action and Preventative Action are implemented to ensure identified non-conformance issues are documented, investigated, and rectified within appropriate timeframes.
Corrective action is any action applied to regain control over a product, process, policy, or procedure that has been identified as being non-conforming or outside nominated limits of acceptability.
Preventative action is any action applied to prevent any identified non-conformance from reoccurring.
The outcome of corrective and preventative actions should result in regained process control after effective application. Specified corrective actions are commonly linked to the HACCP Plans and the food business certification process.
Below are Corrective Action and Preventative Action examples which may be associated with Commercial Sterility Processing related non-conformance:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Corrective Action requirements in relation to their items.
You may wish to visit the Corrective Action and Preventative Action section of haccp.com for examples of best practice applications for this food safety and quality system element.
Verification: The act of reviewing, inspecting, testing, checking, auditing, or otherwise establishing and documenting whether items, processes, services, or documents conform to specified requirements.
Verification is the detailed review of all food safety and quality system elements to confirm that they are effectively developed, documented, implemented, monitored, and reviewed. All food safety and quality system elements, including documented policies, procedures, training, HACCP plans, and their operational applications must be verified on an ongoing scheduled basis. The verification process commonly includes a defined schedule for which verification activities are required, how often they are conducted, who is responsible, and detailed documented procedures for each nominated verification activity.
The general goal of an established verification process is to ensure any systemic non-conformance issues are identified and rectified within an appropriate timeframe. When non-conformance issues are identified through the verification process, Corrective Actions and Preventative Actions should be implemented to ensure they do not impact the effectiveness of the food safety and quality system.
The following examples of verification activities may apply to Commercial Sterility Processing:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Verification requirements in relation to their items.
You may wish to visit the Verification Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.
Validation: The process of gathering evidence to provide a scientific basis for the documented act of demonstrating that a procedure, process, and activity will consistently lead to the expected results. It often includes the qualification of systems and equipment.
Validation is the provision of evidence to support the limits of control or acceptability for food safety or quality parameters nominated within systemic elements. Limits of control or acceptability are commonly included within documented food safety and quality system elements such as procedures, HACCP plans, and specifications.
Common sources of validation include regulatory and legislative standards, finished product specifications and customer requirements, industry codes of practice and guidelines, verified and validated research, historical product, and process control outcomes, and analytical testing.
The general goal of an established validation process is to ensure any inappropriate limits of control or acceptability are identified and rectified within an appropriate timeframe. When non-conformance issues are identified through the validation process, Corrective Actions and Preventative Actions should be implemented to ensure they do not impact the effectiveness of the food safety and quality system.
Validation activities are commonly defined within the verification schedules and procedures of established food safety and quality management systems.
The following examples may apply to validation of the limits of control or acceptability for Commercial Sterility Processing:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Validation requirements in relation to their items.
You may wish to visit the Validation Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.
Skills and Knowledge: Skills and knowledge are attributes of human interactions commonly linked to competency within any specific job-related task.
Training and competency requirements for Commercial Sterility Processing must be ongoing, including regularly scheduled reviews to ensure the effectiveness of training and competency outcomes.
Team members who have defined responsibilities regarding Commercial Sterility Processing should have knowledge including:
Team members who have defined responsibilities regarding Commercial Sterility Processing should have skills including:
Team members who have defined responsibilities regarding Commercial Sterility Processing should have access to resources including:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Commercial Sterility Processing Training, Competency, and Resources requirements in relation to their items.
You may wish to visit the Training, Competency, and Resources section of haccp.com for examples of best practice applications for this food safety and quality system element.