

To define detail, scope and purpose.
To establish the developed detail in a viewable format to facilitate information.
To facilitate the application of the documentation.
Downloading a resource will add this resource to your resource subscriptions. You will be notified of future updates to this resource via email (you may unsubscribe at any time by clicking the unsubscribe link in the email notification, or to unsubscribe immediately from all update notifications, click here)
Downloading a resource will add this resource to your resource subscriptions. You will be notified of future updates to this resource via email (you may unsubscribe at any time by clicking the unsubscribe link in the email notification, or to unsubscribe immediately from all update notifications, click here)
This information can be used to develop food safety and quality programs that meet the requirements of modern Regulatory, Customer and Industry Standards:
When considering the development, documentation, and implementation of Calibration of Measuring and Testing Equipment within food safety and quality management systems, the following information should be considered to ensure effective outcomes:
Inaccurate equipment used to measure or test products or processes can compromise regulatory compliance and the safety and quality of food products. Calibration programs are implemented to ensure that measuring and testing equipment is accurate and capable of meeting its intended requirements.
Calibration is a technique used to confirm that the operational parameters of measuring and testing equipment are accurate. It is usually completed in two steps:
Calibration of Measuring and Testing Equipment involves comparing the readings of a device with those of a reference device, or a specially constructed and certified piece of calibration equipment. Readings are taken at several points across the operating range in which the device will be used (for example, at the ice point and at a hot holding temperature for a thermometer), and the difference from the reference value is recorded. The results allow the accuracy of the device to be assessed and documented as part of the food safety and quality system.
Depending on the type of equipment or device, calibration may be completed internally by the food business, or externally by an appropriate service provider. Calibration is commonly considered a component of the maintenance program.
Measuring and testing equipment that may require scheduled calibration includes:
Additional devices include:
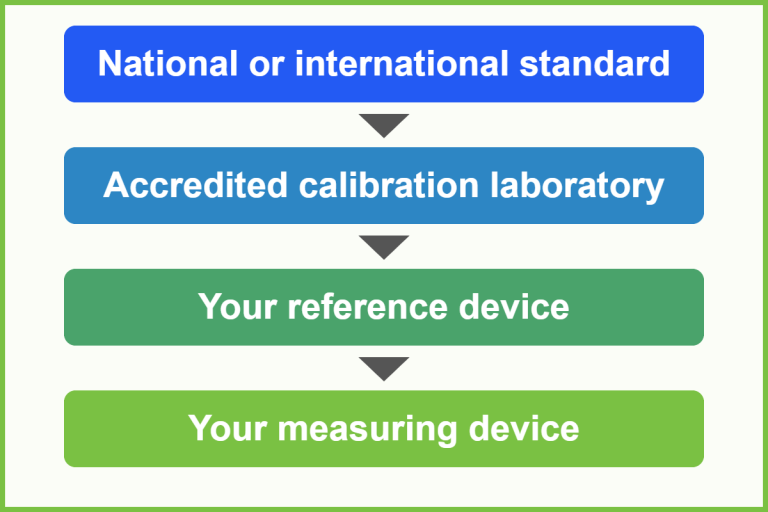
The value of a calibration depends on the reference used. A reference standard should be certified, appropriate for the range and accuracy required, and traceable to national or international standards through an unbroken chain of calibrations. Each step in the chain contributes a stated measurement uncertainty.
Calibration certificates provided by external service providers should be reviewed on receipt. A certificate should typically show:
Where a calibration is critical to food safety or regulatory compliance, it is good practice to use a laboratory accredited to ISO/IEC 17025, and to confirm that the calibration in question is within the laboratory’s scope of accreditation. The terminology used on this page is consistent with the International Vocabulary of Metrology (JCGM 200).
The frequency of calibration should be based on risk. Factors that may be considered include:
Calibration frequencies should be documented in the calibration schedule, and reviewed when results, incidents, or changes in use indicate that a different frequency is appropriate.
Calibration has the obvious benefit of determining whether temperature measuring devices are registering a true temperature reading. For a food safety system to remain verified, it should use temperature measuring devices that can accurately measure the temperature of foods requiring temperature control to within ±1°C (±1.8°F), or within the accuracy specified by relevant regulatory or customer requirements. Where thermometers are calibrated internally, it is important to ensure that the reference thermometer to which other temperature measuring devices are compared is accurate and is calibrated regularly to recognised standards.
Whether monitored by external or internal parties, refrigeration plays a crucial part in any food safety program. The following protocols should be considered regarding the maintenance of refrigerated systems:
Calibration activities can generally be classed as either absolute or local, according to their methods. These terms are used here for continuity; absolute calibration is a traceable calibration with a stated uncertainty, and local calibration is a comparative check completed within the business.
Absolute calibration is when readings are systematically measured against an instrument that has been calibrated by controlled methods and against recognised standards. Governmental authorities and national measurement institutes around the world maintain the scientific standards used to calibrate calibration equipment. Absolute calibration is usually completed in a manner that is traceable to those standards, and its results are reported with a stated measurement uncertainty.
Where it is not possible to perform an absolute calibration, a local calibration, also known as a comparative test, can be performed to ascertain the working accuracy of a measuring or testing device. The reliability of such testing depends on the calibration of the equipment used for comparison and on the control of variables that may alter readings.
Requirements for laboratory testing equipment and materials should include:
Laboratories that perform testing or calibration for others are commonly expected to operate in line with ISO/IEC 17025.
Thermometers are among the most commonly calibrated measuring and testing devices in the food industry. The following are examples of how to complete local calibrations (comparative checks) for contact temperature measuring devices.
Ice point check. Fill an insulated container with crushed ice made from potable water, and add enough clean water to create a slush with ice throughout. Stir the mixture and immerse the thermometer to the depth recommended by the manufacturer, without letting the stem or sensing element touch the bottom or sides of the container. Allow the thermometer display to stabilise for at least a minute, and then read the temperature. The reading should be 0°C (32°F) within the tolerance set for the device.
Boiling point check. Water boils at 100°C (212°F) only at sea level. The boiling point falls as altitude increases, by roughly 1°C (1.8°F) for every 300 m, and varies with atmospheric pressure, so the local boiling point must be determined before this method is used, for example by using a calibrated reference thermometer. Use a vessel that is deep enough to remain unaffected by air cooling, with water at a rolling boil. Place the thermometer probe in the centre of the boiling water without touching the bottom or sides of the container, and allow the display to stabilise for at least a minute before reading. Take all necessary safety precautions to prevent scalding. The ice point check is generally the more reliable method, and boiling point checks are suitable only for devices rated for that temperature.
The reading, the deviation from the expected value, the tolerance, the date, and the person completing the check should be recorded. A device that is outside tolerance should be adjusted, repaired, or removed from use.
For maximum accuracy, temperature measurements have historically been made with devices that contact the food directly. Contact thermometers come in a variety of shapes and sizes and employ various technologies. They all have a contact surface, or probe, that senses the heat of the food it touches. The sensor may be a liquid that expands and contracts; a bimetal, or combination of two different metals that expand or contract at different rates; a thermocouple that generates a small voltage; or a thermistor that varies its electrical resistance, all in proportion to the applied heat. The sensor reacts and the temperature is indicated on a dial, gauge, or display.
The compact size of most of these devices allows them to be carried in a pocket and used readily on a variety of food items. Contact thermometers have drawbacks, the largest of which is a delay in reaction time, and a probe that is not inserted to the correct depth may give an inaccurate reading.
Another consideration is the need to avoid cross-contamination. When taking multiple measurements, probes must be cleaned and sanitised between uses, and users must avoid transferring microorganisms from hands and other surfaces to the food being checked. Infrared thermometers avoid contact with the food, but they have their own limitations, which are described below.
Infrared radiation consists of electromagnetic wavelengths longer than visible light but shorter than microwaves. Infrared thermometers use this radiation to measure surface temperature without contact. To take a reading, the user aims the thermometer at the target, presses a button, and reads the temperature display.
The device has an optical lens that collects the infrared energy radiated from the object and focuses it on a detector. The detector converts the energy into an electrical signal that is amplified and displayed as a temperature reading. The thermometer measures the magnitude of the radiated energy and, using that data and the temperature of the detector, calculates the temperature of the surface that emitted the energy.
Because air is essentially transparent at infrared frequencies, an infrared thermometer can measure food surface temperature without touching the food. This reduces the risk of cross-contamination and avoids the thermal lag of a contact probe that must heat up or cool down after touching food. Infrared thermometers register a surface temperature quickly, which allows many food temperatures to be scanned over a short time as part of general food safety system surveillance.
Accurate temperature measurement is particularly important in the temperature range in which pathogenic bacteria can multiply rapidly, often referred to as the danger zone. The danger zone is commonly described as the range between about 5°C (41°F) and 60°C (140°F), although the exact limits vary between jurisdictions, and local legislation should be followed. If foods requiring temperature control, such as dairy products, seafood, meats, and eggs, remain within this range for more than a short time, bacteria can multiply and produce toxins that may cause foodborne illness. For more information, see Food-Borne Illness Prevention.
A non-contact thermometer can help staff check temperatures quickly, for example when scanning hot and cold holding areas to confirm that foods are at appropriate temperatures. Quick scans can identify potential problems early, and questionable readings can be followed up with a contact thermometer.
Infrared energy is emitted from the surface of the food, and the surface temperature is not always the same as the core temperature. Placing too much reliance on a surface reading is dangerous when the core of the food may remain in the danger zone, as is familiar to anyone who has defrosted or cooked a dense meal in a microwave oven.
Other factors that can affect the accuracy of infrared readings include:
Because of these limitations, regulators commonly do not accept infrared thermometers for enforcement or for demonstrating core temperature compliance. Used as intended by the manufacturer, they are effective screening tools. A reading from an infrared thermometer can be followed by measurement with a contact thermometer whenever questionable readings are obtained, and typical applications include checking surface temperatures of unpackaged, accessible food in hot or cold buffets where multiple consecutive readings are needed.
Users of infrared thermometers play a critical role in the proper and effective operation of the device, so they must be adequately informed about its capabilities and limitations. Information is usually included with each thermometer to help educate users, including:
Further information that users should be aware of includes:
The calibration of fixed devices located in cool rooms and freezers may be completed using the following method, in the nominated sequence:
Although this is a simple method of rating the accuracy of temperature measuring devices, scientifically based principles regarding the correct use of thermometers and other temperature measuring devices must be followed to gain the most accurate results.
Heating units may include:
Calibration of these devices is important, particularly where they are used for hot holding. A common method is to compare the temperature setting or display of the unit with the reading of a calibrated reference probe placed in the working zone, and to confirm that the unit reaches and holds the required temperature. To verify the capability of the devices to hold foods at appropriate temperatures, records of calibration and servicing must be maintained.
Because of the sensitive nature of the operation of these devices, and the potential for foods to become unsafe if they are not held at correct temperatures, it is vitally important that required repairs are carried out before the equipment is used again. Providers of external calibration services should be included within the approved supplier program (see Approved Supplier Management).
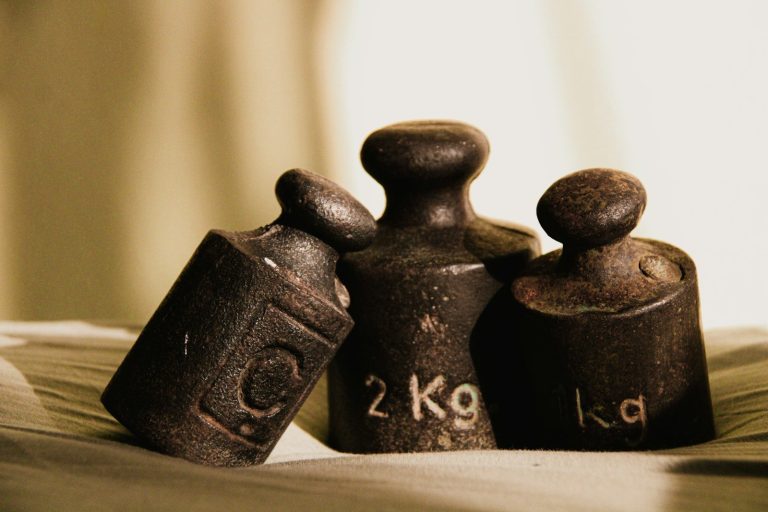
A five-point check of a scale is often used as part of calibration. This is a corner and centre loading (eccentricity) test: first zero the scale, then place a test weight in turn on each of the four corners of the platform and in the middle. The read-out should be the same as the weight at all five positions, within the tolerance set for the scale.
The acceptable tolerance is generally set by the business or customer, based on the product, the risk, and any legal requirements. It should not be set arbitrarily, and the tolerance for scales used for trade or label declarations is defined by weights and measures (legal metrology) requirements.
It is recommended that scales are calibrated by an accredited external service provider at least annually. Weights and measures legislation in many countries and regions requires that scales used for trade are externally certified by an approved or accredited provider. We recommend that you refer to your local weights and measures authority for specific requirements.
Scales can be checked internally using a certified, traceable standard weight reference. The weight chosen should normally be similar to the product weight that the scale is used to measure, and the checks should cover the working range. For example, a 100 g (or ounce) standard weight reference would be appropriate for a scale used to weigh a 110 g (or ounce) product, whereas a 1,000 g (or ounce) weight would not generally be appropriate for that scale.
Internal checks are recommended daily, or at the start of each shift, for scales used to manufacture or sell products by net or gross weight, and whenever a scale has been moved or damaged.
Depending on the type of pH testing device, it may recognise the pH buffer automatically or perform the calibration adjustment automatically. Alternatively, most pH meters can be adjusted manually to ensure that they measure accurately.
It is generally considered best practice for pH meters to be calibrated before each session of use. Each pH testing device is slightly different in its accuracy, and accuracy changes with the age of the electrode. Uncalibrated pH testing devices can give inaccurate results, which may create food safety hazards, particularly where acidity is used to control microbiological growth. Calibration of pH meters is commonly known as pH electrode calibration, because the parameters set depend on the electrode rather than the device.
Calibration of a pH meter calls for two or three pH calibration buffers. These are liquids with a controlled and known pH, and they should bracket the range of pH values expected in the products being tested (for example, pH 4 and 7 for acid foods, or pH 4, 7, and 10 where a wider range is measured). Good practice includes:
In the food processing industry, one of the most common foreign materials found in food is metal. Metal contaminants can be unintentionally introduced to food products and become a safety hazard to consumers. One approach to preventing metal contamination is the use of metal detectors.
Metal detectors can detect metal contaminants such as ferrous metals (iron), non-ferrous metals (such as copper, lead, and brass), and stainless steel. Sensitivity differs between these metal types, and it is also affected by the nature of the product.
Depending on the type of metal detector and the nature of operations, metal detection units are commonly checked by passing certified test pieces through the device using a validated, best practice method. Good practice includes:
The frequency of such checks is determined by risk assessment. Similar principles apply to X-ray inspection systems.
Dosing involves the mixing and application ratios and amounts of the chemicals applied. The critical factor in ensuring foods do not pose a safety risk to consumers in this context is adhering to science-based mixing and application rates. These ratios are usually defined within the chemical manufacturer’s instructions for use, in conjunction with best practice, regulatory, and industry requirements.
Mixing ratios are the dilution rates for chemicals, which are generally mixed with water for application. They are formulated on scientific data to ensure that the chemical application is effective and that the risk of chemical contamination is controlled. Concentrations can be verified with test kits, conductivity meters, or titration.
Application ratios define how much of the diluted chemical is applied within a specific area, or onto a specific crop. These can be justified by the scheduled calibration of chemical application equipment, such as measuring the output of a sprayer over a known area, which may be documented on a Chemical Application Equipment Calibration Log.
If a measuring or testing device is found to be outside the acceptable tolerance, the following steps should be considered:
A device that is found to be out of tolerance should be repaired by the manufacturer or an authorised and approved service provider where applicable. Failure to act promptly could compromise food safety or quality, or breach food law.
Calibration activities should be controlled through an equipment register and calibration schedule. Useful elements include:
Document: A document provides guidance or direction for performing work, making decisions, or rendering judgments that affect the safety or quality of the products or services that customers receive.
Documented policies, procedures, work instructions, and schedules form the basis of any food safety and quality management system. The following documentation formats may be considered to ensure ongoing compliance with specified requirements for Calibration of Measuring and Testing Equipment:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Documentation requirements in relation to their items.
You may wish to visit the Calibration of Measuring and Testing Equipment Templates section of haccp.com for examples of Calibration of Measuring and Testing Equipment documentation, record, and resource formats commonly applied within food safety and quality systems.
Implementation: Implementation is the application of documented food safety and quality system elements into the actual business operation.
The implementation of Calibration of Measuring and Testing Equipment within any food business requires genuine commitment from senior management, staff, contractors, and visitors to ensure the nominated goals of implementation are achievable on an ongoing basis. It is a step that requires significant planning and consideration of general and specific food business circumstances, so that the outcomes of Calibration of Measuring and Testing Equipment do not negatively affect the safety and quality of the food items dispatched from the business.
Implementation of Calibration of Measuring and Testing Equipment must include a clear definition of responsibilities and authorities for all levels of participation by senior management, staff, contractors, and visitors to the site.
When implementing Calibration of Measuring and Testing Equipment within a food safety and quality system, the following requirements may be considered before completion:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Implementation requirements in relation to their items.
Monitoring: Monitoring is the act of reviewing and confirming measurable parameters of a defined process or product status.
Monitoring requirements within food industry sectors are generally identified against limits of acceptability defined within HACCP plans, implementation procedures, and work instructions. Monitoring usually includes some element of record-keeping, which may be maintained manually or through digital systems. Advancements in technology have produced many systems and processes that are self-monitored or self-adjusted when variances are identified. Regardless of the system used, the goal of any monitoring activity is to provide sufficient evidence that any limit of acceptability has been met.
Traditional Calibration of Measuring and Testing Equipment monitoring requirements include manual recording and the application of corrective actions when the results of monitoring are found to be outside acceptable limits. Corrective actions should also be strongly linked to the monitoring process to ensure full traceability of the actions applied.
The following examples of monitoring activities and record formats may be applicable to Calibration of Measuring and Testing Equipment:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Monitoring requirements in relation to their items.
You may wish to visit the Calibration of Measuring and Testing Equipment Templates section of haccp.com for examples of Calibration of Measuring and Testing Equipment documentation, record, and resource formats commonly applied within food safety and quality systems.
Corrective Action: Corrective action is mandatory action to be taken when a deviation from the quality system occurs, particularly concerning a Critical Control Point.
Preventative Action: At any step in the process where a hazard has been identified, preventative action must be put into place to prevent recurrence.
Corrective action and preventative action are implemented to ensure identified non-conformances are documented, investigated, and rectified within appropriate timeframes. Corrective action is any action applied to regain control over a product, process, policy, or procedure that has been identified as non-conforming or outside nominated limits of acceptability. Preventative action is any action applied to prevent an identified non-conformance from recurring.
The outcomes of corrective and preventative actions should result in regained process control after effective application. Specified corrective actions are commonly linked to the HACCP plan and the food business certification process.
Below are corrective action and preventative action examples that may be associated with Calibration of Measuring and Testing Equipment non-conformances:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Corrective Action requirements in relation to their items.
You may wish to visit the Corrective Action and Preventative Action section of haccp.com for examples of best practice applications for this food safety and quality system element.
Verification: The act of reviewing, inspecting, testing, checking, auditing, or otherwise establishing and documenting whether items, processes, services, or documents conform to specified requirements.
Verification is the detailed review of all food safety and quality system elements to confirm that they are effectively developed, documented, implemented, monitored, and reviewed. All food safety and quality system elements, including documented policies, procedures, training, HACCP plans, and their operational applications, should be verified on an ongoing scheduled basis. The verification process commonly includes a defined schedule of the verification activities required, how often they are conducted, who is responsible, and detailed documented procedures for each nominated verification activity.
The general goal of an established verification process is to ensure that any systemic non-conformances are identified and rectified within an appropriate timeframe. When non-conformances are identified through the verification process, corrective actions and preventative actions should be implemented to ensure they do not affect the effectiveness of the food safety and quality system.
The following examples of verification activities may be applicable to Calibration of Measuring and Testing Equipment:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Verification requirements in relation to their items.
You may wish to visit the Verification Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.
Validation: The process of gathering evidence to provide a scientific basis for the documented act of demonstrating that a procedure, process, or activity will consistently lead to the expected results. It often includes the qualification of systems and equipment.
Validation is the provision of evidence to support the limits of control or acceptability for food safety or quality parameters nominated within systemic elements. Limits of control or acceptability are commonly included within documented food safety and quality system elements such as procedures, HACCP plans, and specifications.
Common sources of validation include regulatory and legislative standards, finished product specifications and customer requirements, industry codes of practice and guidelines, verified and validated research, historical product and process control outcomes, and analytical testing.
The general goal of an established validation process is to ensure that any inappropriate limits of control or acceptability are identified and rectified within an appropriate timeframe. When non-conformances are identified through the validation process, corrective actions and preventative actions should be implemented to ensure they do not affect the effectiveness of the food safety and quality system.
Validation activities are commonly defined within the verification schedules and procedures of established food safety and quality management systems.
The following examples may be applicable to the validation of the limits of control or acceptability for Calibration of Measuring and Testing Equipment:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Validation requirements in relation to their items.
You may wish to visit the Validation Activities section of haccp.com for examples of best practice applications for this food safety and quality system element.
Skills and Knowledge: Skills and knowledge are attributes of human interactions commonly linked to competency within any specified job-related task.
Training and competency requirements for Calibration of Measuring and Testing Equipment must be ongoing, including regularly scheduled reviews to ensure the effectiveness of training and competency outcomes.
Team members who have defined responsibilities regarding Calibration of Measuring and Testing Equipment should have knowledge including:
Team members who have defined responsibilities regarding Calibration of Measuring and Testing Equipment should have skills including:
Team members who have defined responsibilities regarding Calibration of Measuring and Testing Equipment should have access to resources including:
If your food business supplies foodstuffs manufactured to a customer’s specifications, it is important to consider any specific Calibration of Measuring and Testing Equipment Training, Competency, and Resources requirements in relation to their items.
You may wish to visit the Training, Competency, and Resources section of haccp.com for examples of best practice applications for this food safety and quality system element.